Astana city, Esil district, Dinmuhamed Konaev street, 25/1. enquiry@karabau.kz +7 707 456 7413

Production & facilities

The refinery structure & process units

From primary crude oil distillation through deep conversion and heavy residue processing, supported by hydrogen production, water supply and a central refinery laboratory.

Process chain

How crude oil becomes finished product

The refinery is configured as a full conversion chain: crude oil is separated, the heavier fractions are upgraded into light products, and residues are converted rather than sold as low-value fuel oil.

Crude oil intake

Oil raw materials from the West Siberian oil fields arrive at the raw feed tank farm.

Primary distillation

Complex of Crude Oil Primary Distillation (LK-6U) separates crude into straight-run fractions.

Advanced processing

Fuel complex KT-1 deep-processes fuel oil, converting residues into light products.

Heavy residue conversion

Delayed Coking, Coke Calcination, Bitumen Production and Sulfur Recovery Units.

Compounding & dispatch

Blending of commercial grades, tank storage and dispatch by rail and road transport.

Main complexes

Principal complexes of the refinery

The structure of the refinery includes a Complex of Crude Oil Primary Distillation (LK-6U), a Complex of Compounding and Oil Products Dispatch, a Complex of Crude Oil Advanced Processing and a Complex of Heavy Oil Residue Processing.

LK-6U

Complex of Crude Oil Primary Distillation

Separates crude oil into straight-run fractions — gasoline, kerosene and diesel cuts plus vacuum gas oil and residuum — which feed every downstream unit. The complex was revamped as part of the upgrading project to increase throughput and improve fractionation quality.
Compounding & dispatch

Complex of Compounding and Oil Products Dispatch

Carries out blending of finished commercial grades to the required specifications and dispatches products to the tank farms and loading facilities. It is the link between process units and the customer.

KT-1

Complex of Crude Oil Advanced Processing

A fuel complex — KT-1 for deep processing of fuel oil. It converts heavy residue into additional light products, raising the refinery's conversion depth. The complex was revamped during the upgrading project.

Heavy residue

Complex of Heavy Oil Residue Processing

Includes several process units such as the Delayed Coking Unit, the Coke Calcination Unit, the Bitumen Production Unit, the Sulfur Recovery Unit and the Sulfur Granulation Unit — converting residues into petroleum coke, bitumen and granulated technical sulfur.

Process units

Units within heavy oil residue processing

Delayed Coking Unit

Delayed Coking

Converts heavy residue into gas oil fractions and petroleum coke using the delayed coking process. Revamped as part of the upgrading project to strengthen residue conversion.

Coke Calcination Unit

Coke Calcination

Further processes raw petroleum coke from the coking unit, raising its carbon quality for industrial and metallurgical applications.

Bitumen Production Unit

Bitumen Production

Produces bitumen of several grades — construction, road and roofing — for road building and industrial use across Kazakhstan.

Sulfur Recovery Unit

Sulfur Recovery

Recovers sulfur from process gas streams, cutting emissions. Commissioned as part of the new Complex of Sulfur Recovery Units in December 2020.

Sulfur Granulation Unit

Sulfur Granulation

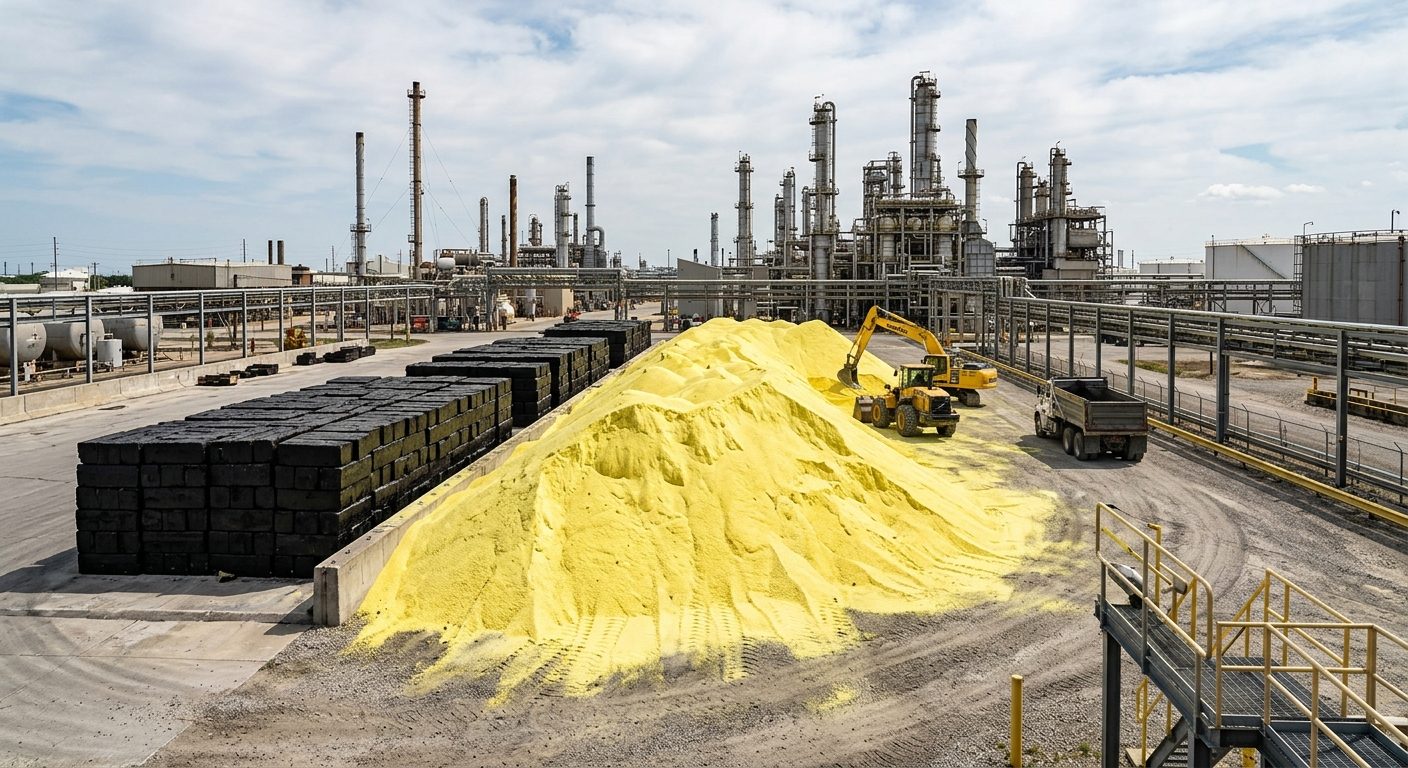
Turns recovered sulfur into granulated technical sulfur — a safe, handleable and marketable by-product for transport and export.

Isomerization & Naphtha Splitter

Isomerization & Naphtha Splitting

New complex commissioned in December 2020 that lifts the octane quality of the gasoline pool through isomerization and naphtha fractionation.

Auxiliary units

Supporting units and site infrastructure

At the refinery there are a Hydrogen Production Unit and an Oil Sludge Processing Unit, as well as large auxiliary units — the Water Supply and Sewerage plant and the Central Refinery Laboratory (CRL).

Hydrogen Production Unit

Supplies hydrogen required for hydrotreating and upgrading, underpinning the production of low-sulphur fuels.

Oil Sludge Processing Unit

Handles oil sludge streams as part of the refinery's environmental and resource-efficiency programme.

Water Supply & Sewerage Plant

A large auxiliary unit ensuring water supply and sewerage for normal operation of the whole complex.

Central Refinery Laboratory (CRL)

Carries out quality control of raw materials, intermediate streams and finished commercial products.

Utilities & offsite facilities

The enterprise has well-developed Utilities & Offsite facilities:

Commodity & Raw Feed Tank Farms

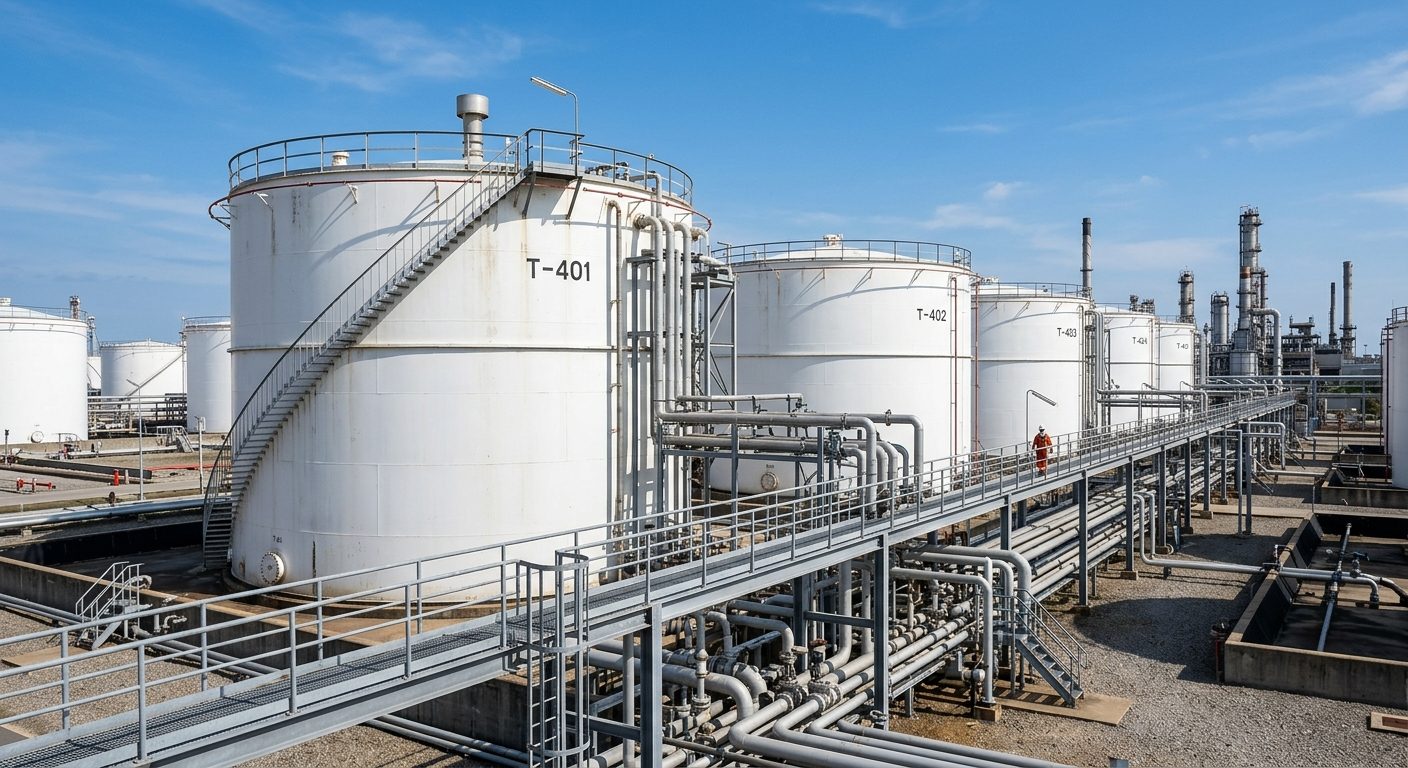
Storage capacity for crude oil raw feed and finished commercial products.

Liquefied Gases Tank Farm

Dedicated storage for hydrocarbon liquefied gases produced by the refinery.

Loading & Unloading Racks

Racks for oil products transportation by rail and road transport.

Upgrading project

What the December 2020 upgrading delivered

As a result of the upgrading project implementation, two new complexes of process units were built and commissioned in December 2020 at the Refinery: the Isomerization and Naphtha Splitter unit and the Complex of Sulfur Recovery Units.

  • Isomerization and Naphtha Splitter unit — built and commissioned December 2020.
  • Complex of Sulfur Recovery Units — built and commissioned December 2020.
  • 12 new U&O facilities built for normal operation of the constructed and brought-into-service units.
  • Revamped existing production capacities: Complex of Crude Oil Primary Distillation, Complex of Crude Oil Advanced Processing and the Delayed Coking Unit.
Outcome: all these measures ensured the production of K-4 motor fuels — diesel and gasoline of RON-92 and RON-95 — in accordance with the requirements of the Technical Regulations of the Customs Union.
White cylindrical crude oil storage tanks in the refinery tank farm Tank farmCommodity & raw feed storage
Granulated technical sulfur and bitumen products at the refinery ProductsTechnical sulfur & bitumen grades

Visit or enquire

Find out more about our production capabilities

For technical product data, volumes and delivery terms, contact our team — we respond to enquiries within one business day.